Category: Uncategorized

  • Building Construction Solutions: The Future of Development

    Building Construction Solutions: The Future of Development

    The way we build is evolving—fast. From towering skyscrapers to smart homes, the future of construction isn’t just about bricks and beams anymore. It’s about technology, sustainability, speed, and innovation. The question is no longer just what we build—but how we build it.

    In this article, we’ll explore the top building construction solutions that are shaping the future of development—solutions that are smarter, faster, and greener than ever before.

    1. Modular & Prefabricated Construction

    Gone are the days of waiting months for a building’s shell. Modular construction involves assembling pre-built sections onsite, drastically cutting down time and cost.

    Key Benefits:

    • Faster project timelines
    • Lower labor costs
    • Less material waste
    • Consistent quality

    🏗️ Think of it like building with giant LEGO blocks—only more precise and much stronger.

    2. Green Building Materials

    Construction is one of the world’s biggest contributors to carbon emissions. The solution? Sustainable materials like:

    • Bamboo (fast-growing and strong)
    • Recycled steel and concrete
    • Hempcrete (a natural, breathable alternative)
    • Low-VOC paints and finishes

    🌍 Build today without borrowing against tomorrow.

    3. 3D Printing in Construction

    Yes, we’re printing buildings now.

    What it offers:

    • Rapid construction of homes and offices
    • Reduced material usage
    • Customization without added labor
    • Lower environmental impact

    🖨️ From concept to concrete in days, not months.

    4. Smart Building Technologies

    We’re no longer just building walls—we’re building brains into our structures.

    Examples include:

    • Automated lighting and HVAC systems
    • Voice-activated home controls
    • Smart energy meters
    • Security systems with facial recognition

    🏢 Buildings that think for themselves.

    5. Energy-Efficient Design

    Modern buildings aren’t just stylish—they’re efficient.

    Key Design Elements:

    • Solar panels and renewable energy integration
    • Double- and triple-glazed windows
    • Passive heating and cooling
    • Insulated panels and green roofs

    💡 Save energy. Save money. Save the planet.

    6. Drones in Construction

    Drones are changing the way we survey and manage construction sites.

    Use Cases:

    • Aerial mapping and inspections
    • Progress tracking
    • Safety monitoring
    • Material delivery in remote areas

    🚁 Fewer boots on the ground. More eyes in the sky.

    7. Building Information Modeling (BIM)

    BIM is like Google Docs for buildings—everyone involved can see, edit, and interact with the structure in real time before it’s built.

    Advantages:

    • Better coordination
    • Fewer errors
    • Cost savings
    • 3D visualization of the entire project

    🧠 Design it digitally, then bring it to life.

    8. Robotics and Automation On-Site

    Robots can now:

    • Lay bricks
    • Pour concrete
    • Install drywall
    • Paint walls

    🤖 They don’t need coffee breaks and don’t make mistakes.

    9. Sustainable Urban Planning

    Future development isn’t just about buildings—it’s about building communities.

    Focus Areas:

    • Mixed-use developments
    • Walkability
    • Green spaces
    • Public transport integration

    🏙️ Cities that work for people, not just profit.

    10. Resilient and Disaster-Proof Structures

    As climate events grow more extreme, we need buildings that stand the test of nature.

    Solutions:

    • Flood-resistant foundations
    • Earthquake-proof materials
    • Fire-retardant building envelopes

    🌪️ Build once, withstand anything.

    Conclusion

    From 3D-printed homes to AI-powered design tools, construction is undergoing a revolution. But this isn’t just about speed or technology—it’s about creating spaces that are sustainable, safe, and smarter for the generations to come.

    The future of development depends on how boldly—and wisely—we adopt these construction solutions today.

  • Road Safety Solutions: Your Guide to Safer Travels

    Road Safety Solutions: Your Guide to Safer Travels

    Traveling—whether it’s a short commute or a long road trip—shouldn’t feel like a gamble. But every day, accidents, poor road conditions, and distractions put millions at risk. The good news? We’re not powerless.

    This guide will walk you through road safety solutions that actually work—some high-tech, others surprisingly simple—all aimed at helping you, your family, and everyone on the road travel safer.

    1. The Power of Planning Ahead

    Ever heard the saying “Failing to plan is planning to fail”? It’s true on the road. Safe travel starts before you even buckle up.

    • Check weather and road conditions
    • Ensure your vehicle is roadworthy (tires, brakes, lights)
    • Plan routes with safer, well-lit roads
    • Avoid driving during fatigue-prone hours

    ⛽ Think of it like pre-flight checks—but for your car.

    2. Defensive Driving Techniques

    Being a defensive driver means:

    • Expecting the unexpected
    • Keeping a safe distance from other vehicles
    • Watching for erratic drivers
    • Avoiding distractions (yes, that means your phone)

    🧠 Stay alert. Stay alive.

    3. Seat Belts: Still the MVP of Safety

    Simple? Yes. But seat belts reduce the risk of fatal injury by 45–60%, depending on the vehicle. Make it a non-negotiable rule—for everyone in the car, every time.

    Even in the back seat.

    4. Smart Vehicle Features That Help

    Modern cars are full of built-in safety tech. Some top examples:

    • Automatic emergency braking
    • Lane departure warnings
    • Blind spot detection
    • Rear cross-traffic alerts

    Don’t just drive—let your car help you drive smarter.

    5. Motorcycle & Bike Safety Measures

    Two-wheelers are more vulnerable. Key safety practices include:

    • Wearing proper helmets (DOT-certified)
    • Using reflective gear
    • Riding in visible lanes
    • Keeping headlights on, even during the day

    🚲 Visibility = survival.

    6. Safer Roads Start with Better Infrastructure

    Governments and city planners have a role too. Effective solutions include:

    • Clearly marked pedestrian crossings
    • Speed bumps in residential zones
    • Roundabouts to reduce collision points
    • Lighting in high-risk areas

    📍 You can drive perfectly and still be at risk if roads aren’t designed for safety.

    7. Smart Traffic Management Systems

    Traffic control has gotten a tech upgrade. Cities now use:

    • AI-based traffic signal timing
    • Real-time road alerts and updates
    • Smart cameras to enforce traffic rules
    • Digital speed display signs to nudge drivers

    🌐 Tech that adapts to traffic makes roads safer for everyone.

    8. Pedestrian Awareness Campaigns

    We often talk about drivers—but pedestrians need guidance too. Road safety education for walkers and cyclists includes:

    • Teaching safe crossing habits
    • Encouraging phone-free walking
    • Highlighting nighttime visibility tips

    🦺 Road safety is everyone’s job.

    9. Vehicle Maintenance = Accident Prevention

    A poorly maintained vehicle is a hazard. Routine checks prevent:

    • Brake failures
    • Tire blowouts
    • Headlight malfunctions
    • Steering issues

    🚗 Treat your car like you treat your health—routine checkups save lives.

    10. Emergency Preparedness While on the Road

    Sometimes, things still go wrong. Are you ready?

    Keep in your vehicle:

    • A first-aid kit
    • Reflective triangles or flares
    • A flashlight
    • Phone charger and emergency contacts

    🔦 When minutes matter, being prepared can make all the difference.

    Conclusion

    Whether you’re walking, driving, or cycling—safety is never someone else’s problem. It’s something we create together, through better habits, smarter tools, and a deeper awareness of the risks.

    Use this guide not just for yourself, but to inspire your family, friends, and community. Because the best journey is the one where everyone arrives safely.

  • 7 Essential Road Safety Solutions You Need to Know

    7 Essential Road Safety Solutions You Need to Know

    Every time we get behind the wheel, ride a bike, or cross the street, we’re trusting that everyone’s following the rules. But with growing traffic, distracted driving, and tech-heavy vehicles, road safety is more crucial than ever.

    So, what are the most essential road safety solutions we should all be aware of? Let’s break it down into 7 must-know strategies that are helping save lives and make our roads safer.

    Top 7 Essential Road Safety Solutions

    1. Smart Traffic Signals

    Gone are the days of simple timers. Modern smart traffic lights use sensors and AI to:

    • Adapt to real-time traffic flow
    • Prioritize emergency vehicles
    • Reduce waiting times

    Think of it as the brain of the road network—constantly learning and improving.

    2. Advanced Driver Assistance Systems (ADAS)

    These systems are built into many modern cars and act like a digital co-pilot. Some common features include:

    • Lane-keeping assist
    • Automatic emergency braking
    • Blind spot monitoring
    • Adaptive cruise control

    ADAS helps prevent human error—which is responsible for over 90% of accidents.

    3. Pedestrian-Friendly Infrastructure

    It’s not just about drivers. Roads need to be designed for everyone, especially pedestrians and cyclists. Key improvements include:

    • Raised crosswalks
    • Countdown timers
    • Dedicated bike lanes
    • Pedestrian islands in wide roads

    The safer people feel walking, the more they’ll walk. And that’s better for health and the environment too.

    4. Vehicle-to-Everything (V2X) Communication

    Sounds futuristic? It’s happening now. V2X allows vehicles to communicate with:

    • Other vehicles (V2V)
    • Traffic systems (V2I)
    • Pedestrians’ smartphones (V2P)

    This tech helps cars “see” things drivers can’t—like a car suddenly braking two vehicles ahead.

    5. Speed Control Technologies

    Speed kills. But technology is stepping in to help:

    • Speed limiters that cap how fast a vehicle can go
    • Speed cameras with AI to catch violations instantly
    • Geofencing for school zones or construction areas

    Even simple digital speed signs can make drivers hit the brakes.

    6. Enhanced Road Markings and Signage

    You’d be surprised how much difference clear road markings make. Today’s solutions include:

    • Reflective and glow-in-the-dark paint
    • LED-embedded signage
    • Digital warning boards for accidents or bad weather

    Simple, low-tech changes can have big impacts when done right.

    7. Driver Education & Awareness Campaigns

    All the tech in the world can’t replace a well-informed, responsible driver. That’s why regular:

    • Defensive driving courses
    • Anti-distracted driving campaigns
    • DUI prevention efforts

    …are still some of the most powerful tools we have. Education saves lives.

    Check Now :- List Of Road Safety Products

    Conclusion

    These 7 road safety solutions are changing how we drive, ride, and walk. Whether it’s AI-powered traffic lights or a reminder to wear your seatbelt, it all matters. The more we use these tools—and understand them—the safer our roads become.

    Ready to drive change? Contact us today for custom road safety solutions tailored to your needs—together, we can save lives.

  • 8 Key Features of  Effective Industrial Warehouse Solutions

    8 Key Features of Effective Industrial Warehouse Solutions

    In today’s fast-paced industrial environment, efficient warehouse management isn’t just a nice-to-have—it’s mission-critical. Whether you’re a manufacturer, distributor, or e-commerce brand, your warehouse is the beating heart of your operations.

    But not all warehouse solutions are created equal.

    So what separates a basic warehouse setup from an effective, future-ready industrial warehouse solution? Let’s break down the eight key features that truly make a difference.

    What Makes an Industrial Warehouse Solution “Effective”?

    An effective industrial warehouse solution is one that delivers:

    • Speed and efficiency
    • Scalability for future growth
    • Seamless tech integration
    • Reduced costs and increased accuracy

    It’s not just about storing goods—it’s about streamlining your entire supply chain.

    8 Key Features of Effective Industrial Warehouse Solutions

    1. Scalability and Flexibility

    Industrial operations aren’t static—they scale with demand, seasons, and markets.

    Why it matters:

    • Modular warehouse systems can grow with your business
    • Flexibility to shift layouts, zones, and workflows without major overhauls

    Think of it like LEGO blocks for logistics—easy to add, rearrange, or optimize.

    2. Integration with Warehouse Management Systems (WMS)

    Your warehouse should talk to your business systems. A robust WMS is the brain of the warehouse.

    Key benefits:

    • Real-time inventory updates
    • Automatic order processing
    • ERP and e-commerce platform integration

    This means fewer errors, faster decisions, and a more connected supply chain.

    3. Automation and Robotics

    Manual processes are slow and error-prone. Automation changes the game.

    Includes:

    • Conveyor belts
    • Autonomous Mobile Robots (AMRs)
    • Robotic arms for picking and packing

    You get faster order fulfillment, lower labor costs, and 24/7 productivity.

    4. Efficient Layout and Space Optimization

    A smart warehouse doesn’t just hold more—it holds better.

    Techniques include:

    • Vertical storage with AS/RS (Automated Storage and Retrieval Systems)
    • Narrow aisle racking
    • Smart floor planning

    This reduces the need for expansion while maximizing every square foot.

    5. Real-Time Inventory Tracking

    Guessing is risky. With IoT-enabled solutions, you always know what’s in stock.

    Benefits:

    • Prevents overstock and stockouts
    • Improves order accuracy
    • Enables fast reordering and forecasting

    Sensors, RFID tags, and barcode scanners do the heavy lifting here.

    6. Safety and Compliance

    Industrial warehouses must meet strict safety standards—and a good solution ensures they do.

    Focus areas:

    • Ergonomic design for workers
    • Fire detection/suppression systems
    • Adherence to ISO and local compliance standards

    Safety isn’t just ethical—it protects your bottom line.

    7. Energy Efficiency and Sustainability

    Eco-friendly operations are becoming the norm.

    Green warehouse features:

    • LED lighting and energy-saving HVAC
    • Solar power integration
    • Low-energy conveyors and electric forklifts

    Not only is this good for the planet, but it also cuts operational costs.

    8. Advanced Analytics and Reporting

    What’s working and what’s not? Data tells the story.

    Capabilities:

    • Track KPIs like order accuracy, inventory turnover, and picking speed
    • Use AI to forecast demand or prevent bottlenecks
    • Improve processes continuously based on insights

    This is your roadmap to long-term efficiency and ROI.

    Technologies Behind These Features

    The magic behind effective warehousing lies in the tech stack:

    • AI & ML – Predict demand and optimize resources
    • IoT – Real-time tracking and smart alerts
    • Cloud WMS – Centralized control from anywhere
    • AMRs – Navigate and transport goods autonomously
    • Big Data Analytics – Improve decision-making

    Choosing the Right Warehouse Solution Provider

    Before you commit, ask:

    • Do they offer customization?
    • Is their tech future-proof?
    • Can they scale with your needs?

    Red flags:

    • No post-implementation support
    • Outdated software
    • Lack of integration with your systems

    Choose a partner, not just a vendor.

    Conclusion

    Industrial warehouse solutions are no longer just about racks and forklifts. In a competitive landscape, the winners are those who automate smart, track in real-time, use data for growth, and build scalable systems.

    Whether you’re starting small or expanding fast, investing in the right features today will keep your operations lean, agile, and profitable tomorrow.

  • Exploring the Benefits of Warehouse Automation Solutions

    Exploring the Benefits of Warehouse Automation Solutions

    Warehouses are the heart of supply chains—and they’re getting smarter every day. As customer expectations climb and delivery timelines shrink, traditional manual processes just can’t keep up. That’s where warehouse automation comes in.

    Across India and beyond, businesses are investing in automation to scale, speed up, and smarten their operations. But what exactly does automation do, and why is everyone talking about it? Let’s dive in.

    What is Warehouse Automation?

    At its core, warehouse automation is about replacing repetitive, manual tasks with technology. This can be hardware like robots and conveyor belts or software like AI and warehouse management systems (WMS).

    Types of Warehouse Automation:

    • Basic Automation: Conveyor belts, barcode scanners
    • Advanced Automation: AI, robotics, drones
    • Software Automation: Inventory management, order tracking, real-time data dashboards

    Key Benefits of Warehouse Automation

    1. Increased Operational Efficiency

    Automated systems can pick, sort, and pack items in a fraction of the time humans take. They also work around the clock, which means faster throughput without downtime.

    2. Reduced Labor Costs

    Labor is one of the largest expenses in warehouse operations. With automation:

    • You reduce the number of staff required for routine tasks
    • Human workers can shift to roles requiring creativity or decision-making

    3. Improved Accuracy and Fewer Errors

    Ever had the wrong product shipped to a customer?
    With robotics and barcode scanning, such errors are drastically reduced. Automation brings precision to every step of the process.

    4. Enhanced Safety and Ergonomics

    Machines can handle heavy lifting, dangerous environments, or repetitive tasks—keeping human workers safer. This leads to fewer workplace injuries and lower insurance costs.

    5. Real-Time Inventory Visibility

    Thanks to IoT devices and WMS integration, businesses now have up-to-the-minute visibility on stock levels, order status, and shelf life. No more guesswork.

    6. Scalability and Flexibility

    Need to ramp up for the holiday season or handle unexpected spikes in orders?
    Modular automation systems grow with your needs—no need to rebuild your entire warehouse.

    7. Better Space Utilization

    Automation enables vertical stacking and efficient aisle planning. With AS/RS systems, even tight spaces can hold massive inventory, freeing up real estate costs.

    8. Faster Order Fulfillment

    In the age of same-day delivery, speed is king. Automation ensures:

    • Shorter order-to-dispatch time
    • Minimal picking/packing delays

    9. Data-Driven Decision Making

    Automated systems collect and analyze data on every movement in the warehouse. Use this data to:

    • Optimize workflows
    • Predict demand
    • Reduce waste

    10. Competitive Advantage

    Brands that automate stay ahead of the curve—delivering faster, better, and more consistently than their manual competitors.

    Technologies Powering These Benefits

    • Warehouse Management Systems (WMS): Manages inventory, order processing, shipping, and storage zones. Often integrated with ERP systems.
    • Autonomous Mobile Robots (AMRs): Move inventory from one point to another—no human intervention needed.
    • Conveyor & Sorting Systems: Efficiently transport and route products to the correct packing stations.
    • Internet of Things (IoT): Tracks temperature, humidity, product location, and machine status in real time.

    Challenges and Considerations

    • Upfront Investment: Automation requires a significant initial spend. However, the ROI often justifies the cost within 2–3 years.
    • Workforce Training: Shifting from manual to automated workflows requires proper training, change management, and sometimes a cultural shift in operations.
    • Integration with Legacy Systems: Old ERP systems might not “talk” well with modern automation tools. Ensuring seamless integration is key to success.

    Is Warehouse Automation Right for Your Business?

    If your operations involve:

    • Repetitive tasks
    • High error rates
    • Seasonal volume spikes
    • Pressure to reduce costs

    Conclusion

    Warehouse automation isn’t a trend—it’s a transformation. With tangible benefits like speed, accuracy, safety, and cost-efficiency, it’s becoming the cornerstone of modern logistics.

    Whether you’re a small startup or a large enterprise, adopting warehouse automation solutions can put you ahead of the curve, delight your customers, and future-proof your business.

  • Top Automated Industrial Warehouse Solutions in India

    Top Automated Industrial Warehouse Solutions in India

    Warehouse automation in India is no longer a futuristic dream—it’s here, growing, and redefining how businesses operate. From bustling e-commerce giants like Flipkart to traditional manufacturers transitioning into smart factories, automation is fueling efficiency, accuracy, and profitability.

    With India’s industrial sectors expanding rapidly, the need for scalable, intelligent, and cost-effective warehousing solutions has skyrocketed. Let’s explore the top players, the tech behind it, and why automated warehousing is the future of logistics in India.

    What is Warehouse Automation?

    Warehouse automation refers to the use of technology—like robotics, AI, and software systems—to perform tasks traditionally done by humans. These tasks range from inventory tracking to picking, packing, transporting, and storing goods.

    Types of Warehouse Automation:

    • Basic Automation – Conveyors, sorting systems
    • Advanced Automation – Robotics, AS/RS, autonomous vehicles
    • Software Automation – WMS, AI algorithms, predictive analytics

    Benefits of Automated Warehouse Solutions

    Why are Indian industries racing toward automation?

    • Boosted Efficiency – Robots don’t tire, and AI never sleeps.
    • Lower Operational Costs – Reduced dependency on manual labor.
    • Better Accuracy – Minimized human errors in picking and shipping.
    • Real-time Inventory Management – Always know what’s in stock.

    Key Drivers of Automation in India

    • E-commerce Boom – Same-day delivery is impossible without automation.
    • Rising Expectations – Consumers demand speed and accuracy.
    • Labor Challenges – High attrition rates and training costs.
    • Make in India – Push for modernization of infrastructure and logistics.

    Top Automated Warehouse Solutions in India

    1. Grey Orange

    Grey Orange is a pioneer in warehouse robotics, offering intelligent systems that integrate robots with AI. Their Butler robots and Grey Matter™ software form a flexible solution that adapts to real-time demands.

    2. Addverb Technologies

    This Noida-based company builds innovative robotics-based solutions like Dynamo (AMRs), Quadron (Carton shuttles), and Veloce (pallet shuttles).

    3. Godrej Consoveyo

    A division of Godrej & Boyce, this company provides comprehensive automation for warehouses with a focus on AS/RS, cranes, and conveyor solutions.

    4. Falcon Autotech

    Falcon Autotech designs highly modular and scalable sorting and scanning systems. Their DWS (Dimension, Weigh, Scan) solutions are widely used by e-commerce firms.

    5. Mahindra Logistics

    Mahindra is moving beyond trucks and warehouses to build automated fulfillment centers, leveraging AGVs (automated guided vehicles), IoT, and AI tools.

    6. Gati-KWE

    With Japanese logistics partner Kintetsu, Gati has introduced cutting-edge warehouse systems using robotics, automated storage, and real-time tracking.

    Technologies Powering Warehouse Automation in India

    🧠 Artificial Intelligence (AI) & Machine Learning

    AI helps warehouses predict order patterns, optimize routes, and even reassign robots in real time for max efficiency.

    📡 Internet of Things (IoT)

    From smart sensors that track package conditions to real-time equipment diagnostics, IoT is the digital backbone of modern warehouses.

    🤖 Robotics

    Robots—whether they’re AMRs, AGVs, or robotic arms—are the workhorses of the automated warehouse, handling tasks with speed and precision.

    🏗️ Automated Storage and Retrieval Systems (AS/RS)

    These are mechanized systems for automatically placing and retrieving loads. They’re fast, accurate, and save massive floor space.

    🧾 Warehouse Management Systems (WMS)

    WMS software manages everything from stock locations to order tracking, helping businesses keep tight control over operations.

    ⚠️ Challenges in Implementing Warehouse Automation

    💰 High Initial Costs

    Robots and AI systems are expensive upfront, even if they pay off in the long run.

    👷 Skill Gap

    Many workers are unfamiliar with the new tech, and retraining takes time and money.

    🧩 Legacy System Integration

    Not all older warehouses are ready for smart tech. Integrating old and new systems can be a nightmare.

    🔮 Future of Warehouse Automation in India

    India’s warehousing future is smart, sustainable,

    and software-driven. Expect the integration of 5G, blockchain for secure supply chains, and green automation to dominate in the coming years.

    Also, look out for the rise of micro-fulfillment centers in urban areas for faster last-mile delivery.

    ✅ Conclusion

    Warehouse automation is no longer a luxury—it’s a necessity. With rising demand, complex supply chains, and fierce competition, businesses in India are increasingly turning to automation to stay ahead. Whether it’s AI-driven robots or IoT-connected systems, the future belongs to those who automate smart and scale fast.

  • Different Types of Industrial Automation

    Different Types of Industrial Automation

    Ever wondered how factories keep producing at lightning speed without missing a beat? The answer lies in industrial automation. But here’s the twist—it’s not a one-size-fits-all solution. There are different types of industrial automation, each designed to suit specific production needs.

    Whether you’re in manufacturing, food processing, or any industry that runs on machines, understanding these types will help you choose the best path for scaling up. Let’s break it all down.

    What is Industrial Automation?

    Before diving into the types, here’s a quick refresher:
    Industrial automation refers to using machines, control systems, and software to handle industrial processes—minimizing or eliminating human involvement.

    The main goals? Boost productivity, reduce error, cut costs, and improve safety.

    Why Understanding the Types Matters?

    Choosing the wrong type of automation is like using a bulldozer to crack a walnut—it’s overkill and costly. Knowing the different types helps you:

    • Select the right solution for your business
    • Optimize efficiency and cost
    • Stay competitive and scalable

    The Four Main Types of Industrial Automation

    1. Fixed (Hard) Automation

    What Is It?

    Also known as hard automation, this type is designed for high-volume, repetitive tasks. The setup is rigid and tailored for one specific process.

    Common Applications:

    • Automotive assembly lines
    • Bottling and packaging in food production
    • Metal stamping

    Pros:

    • Super-fast production
    • Low per-unit cost (after setup)
    • Consistent output quality

    Cons:

    • Zero flexibility
    • High initial cost
    • Time-consuming to reprogram or reconfigure

    Best For:

    Companies that mass-produce a single product for a long period.

    2. Programmable Automation

    What Is It?

    As the name suggests, programmable automation can be reprogrammed for different tasks. It’s ideal for batch production—where one product is made for a time and then the system switches to another.

    Common Applications:

    • Electronics assembly
    • Textile manufacturing
    • Injection molding

    Pros:

    • More flexible than fixed automation
    • Suitable for varying product types
    • Medium-volume production capabilities

    Cons:

    • Changeovers take time and planning
    • Higher cost per unit than fixed automation

    Best For:

    Businesses producing multiple product models in batches.

    3. Flexible (Soft) Automation

    What Is It?

    Flexible automation is the next level of programmable automation. It allows for quick and easy changeovers, often automatically, making it ideal for dynamic production environments.

    Common Applications:

    • Custom manufacturing
    • Advanced robotics systems
    • Consumer electronics

    Pros:

    • Extremely adaptable
    • Fast product changeovers
    • Reduces downtime

    Cons:

    • High cost to implement
    • Requires skilled personnel

    Best For:

    Industries needing frequent design changes and low to medium batch sizes.

    4. Integrated Automation

    What Is It?

    This refers to a fully integrated system where machines, software, sensors, and control systems work seamlessly together. It’s a smart factory model, often associated with Industry 4.0.

    Common Applications:

    • Smart manufacturing
    • Continuous production systems
    • High-tech industries

    Pros:

    • Full automation and connectivity
    • Real-time data and monitoring
    • Optimized efficiency and quality control

    Cons:

    • High upfront cost
    • Complex to implement and maintain

    Best For:

    Large, tech-savvy companies ready to invest in long-term gains and full digital transformation.

    Bonus: Emerging Types of Automation

    Technology doesn’t stand still, and neither does automation. Here are two emerging types to keep an eye on:

    Collaborative Automation (Cobots)

    Cobots are designed to work safely alongside humans, assisting in tasks like material handling, inspection, and light assembly. They offer flexibility and cost-efficiency for small to medium enterprises.

    Hyperautomation

    This is a broader concept that combines AI, ML, robotic process automation (RPA), and more to automate everything possible across an organization—not just the shop floor.

    Comparison Table: Types of Industrial Automation

    Type Flexibility Volume Cost Changeover Time Best For
    Fixed Automation Low High High Long Mass production
    Programmable Medium Medium Medium Moderate Batch production
    Flexible High Low-Medium High Fast Custom manufacturing
    Integrated Very High High Very High Real-time Smart, connected factories

    How to Choose the Right Type

    Ask yourself:

    • What’s your production volume?
    • How often do you change product designs?
    • What’s your budget and technical capacity?
    • Do you need real-time data and smart systems?

    Understanding your unique business needs is key to selecting the right automation strategy.

    Conclusion

    Industrial automation isn’t just about machines doing the work—it’s about choosing the right kind of machines, systems, and software for your specific needs.

    From fixed automation for high-volume production to flexible and integrated systems for dynamic operations, each type offers unique advantages. By understanding them, you can future-proof your operations and unlock new levels of productivity, safety, and efficiency.

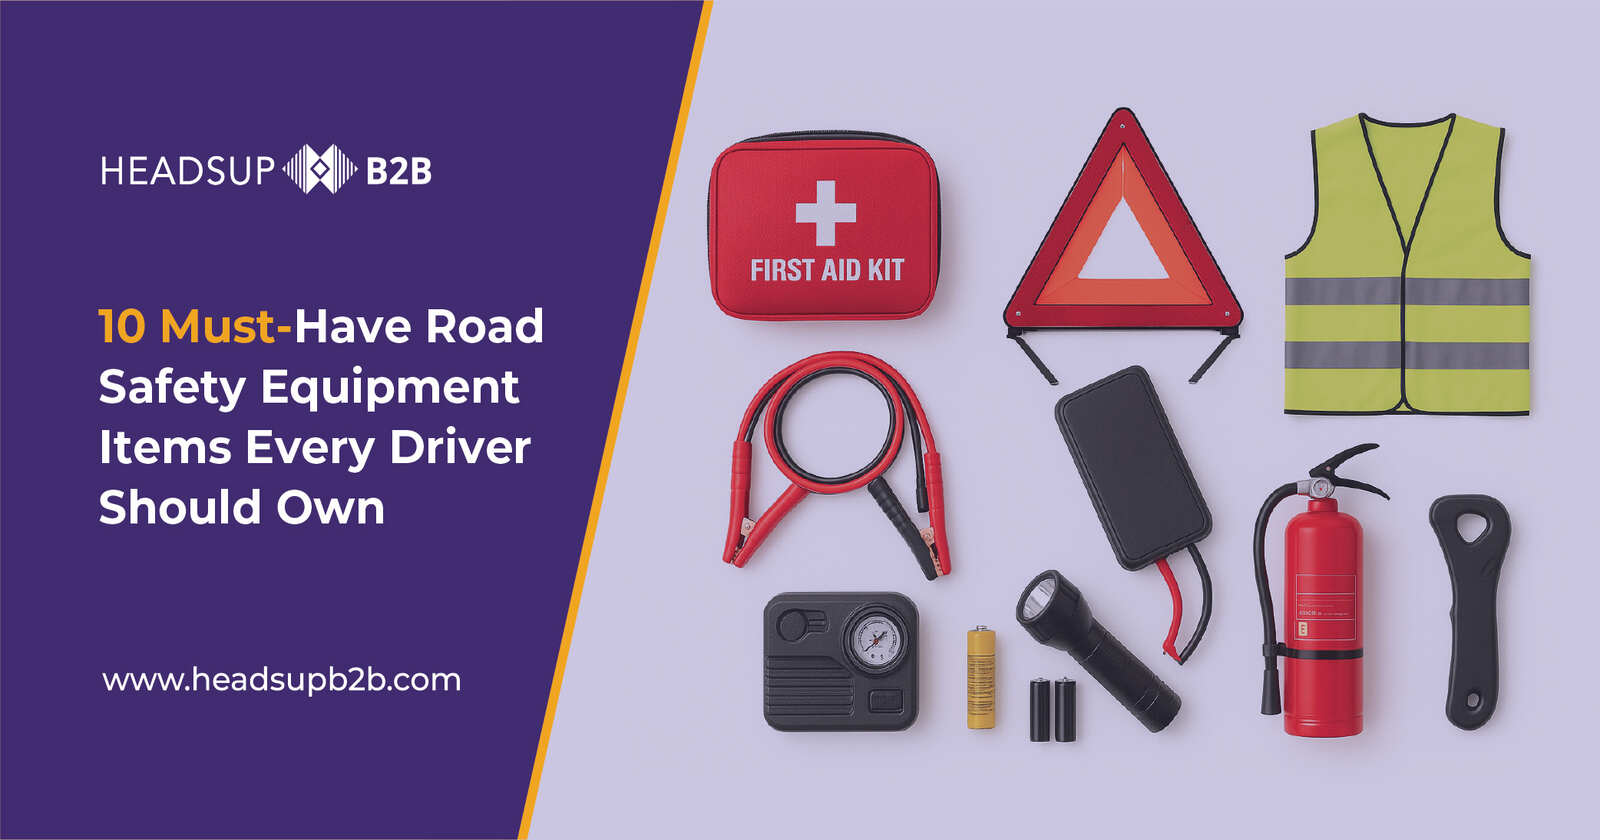
  • 10 Must-Have Road Safety Equipment Items Every Driver Should Own

    10 Must-Have Road Safety Equipment Items Every Driver Should Own

    Let’s face it — no one plans to break down on a deserted highway in the middle of the night. But guess what? It happens. Whether you’re heading out for a long road trip or just running errands, being prepared can be the difference between a minor inconvenience and a full-blown disaster. That’s why every driver should have a set of road safety essentials in their vehicle — no excuses.

    So what exactly should you be keeping in your trunk or glove compartment? Let’s break it down.

    The Top 10 Must-Have Road Safety Items

    1. First Aid Kit

    Think of this as your mobile medical cabinet. Cuts, scrapes, burns — you never know when someone might need a quick patch-up.

    What to include:

    • Bandages and gauze
    • Antiseptic wipes
    • Pain relievers
    • Tweezers and scissors
    • Gloves and a CPR mask

    Why it matters: A first aid kit can be a literal lifesaver, especially in remote areas or before medical help arrives.

    2. Reflective Warning Triangles

    If your car breaks down, these little guys alert other drivers of your presence — especially in low visibility conditions.

    How to use: Set up one 50 to 100 feet behind your car. If you’re on a highway, place one in front as well.

    Pro Tip: Some countries actually require them by law. Better safe than sorry!

    3. High-Visibility Safety Vest

    Ever tried flagging down help at night wearing dark clothes? Not a good idea.

    Why you need one: It ensures you’re visible to other drivers — especially important if you have to step out on a busy road.

    4. Jumper Cables or a Portable Jump Starter

    Batteries die. It’s a fact of life. But being stranded because of one doesn’t have to be.

    What’s the difference?

    • Jumper cables need another vehicle.
    • Jump starters don’t — they come with built-in power.

    Pick your fighter depending on how often you drive solo.

    5. Fire Extinguisher

    Sounds dramatic? Maybe. But car fires happen more than you’d think — especially with overheating or electrical issues.

    Choose a type:
    Look for a Class B or C extinguisher, which is ideal for flammable liquids and electrical fires.

    Keep it accessible, not buried under your golf clubs.

    6. Tire Repair Kit and Inflator

    Flat tire with no spare? You’ll thank yourself for packing this.

    What’s inside?

    • Sealant to temporarily patch the hole
    • A portable inflator to reinflate your tire

    Note: It’s a temporary fix — just enough to get you to a repair shop.

    7. Flashlight with Extra Batteries

    Your phone’s flashlight won’t cut it forever — especially if your battery’s dying.

    Go LED: They’re brighter, last longer, and are more energy-efficient.

    Bonus Tip: Store it where you can reach it without getting out of the car.

    8. Seatbelt Cutter and Window Breaker

    Ever seen a car submerged in water in the movies? It’s real — and terrifying.

    This tool can save your life if your seatbelt gets jammed or the doors won’t open.

    Compact and cheap, there’s no excuse not to have one.

    9. Emergency Blanket

    Looks like a shiny piece of foil, but don’t underestimate it.

    Purpose: Keeps you warm if you’re stuck in cold weather — like a space-age sleeping bag.

    Lightweight, cheap, and folds up small. Just do it.

    10. Multi-tool or Car Emergency Tool Kit

    Think of it as the Swiss Army knife of the road.

    Typical features:

    • Pliers
    • Screwdrivers
    • Wire cutters
    • Glass breaker
    • Knife

    Why it rocks: One tool, many uses. Perfect for quick fixes on the go.

    Additional Safety Essentials Worth Considering

    Beyond the essentials, here are a few extras you’ll be glad you packed:

    • Portable power bank or car charger
    • Bottled water and non-perishable snacks
    • Printed road maps (because tech fails too)
    • Rain poncho or umbrella
    • Towel or rag

    These might not save your life, but they sure can save your day.

    How to Properly Store Your Safety Equipment

    Having the gear is one thing. Being able to find it when needed is another.

    • Use a dedicated storage box in your trunk
    • Keep essential items like flashlights and tools within arm’s reach
    • Avoid clutter — only keep what you truly need

    In some regions, certain items are legally required, like reflective triangles and vests.

    Insurance tip:
    Being well-equipped shows responsibility. It can even help during claims — especially if your preparedness reduced damages or injuries.

    Tips for Keeping Your Road Safety Kit Up to Date

    Don’t just toss it in your trunk and forget about it.

    • Check every 6 months
    • Replace expired items like meds and batteries
    • Test tools like your flashlight or jump starter

    Make it a habit — like your oil change or tire rotation.

    Real-Life Roadside Emergency Scenarios

    Let’s get real — these aren’t just “what ifs.” Here’s how having the right gear made a difference:

    • Flat tire at midnight? Tire inflator to the rescue.
    • Battery dead in the mall parking lot? Jump starter saved the day.
    • Stuck in a blizzard? Emergency blanket and snacks = lifesaver.

    Bottom line? These aren’t just tools — they’re peace of mind.

    Conclusion

    Being prepared isn’t paranoid — it’s smart. Whether you’re a new driver or a seasoned road warrior, these 10 must-have Road Safety Equipment can turn a potential disaster into a manageable hiccup. Don’t wait for something to go wrong. Load up, pack smart, and drive safe.

  • Industrial Warehouses and Their Management: Everything You Need to Know

    Industrial Warehouses and Their Management: Everything You Need to Know

    Industrial warehouses are the backbone of global supply chains. Whether it’s raw materials for factories or finished goods for retailers, everything passes through these storage powerhouses. But with massive inventories, high-speed operations, and increasing demand for efficiency, managing an industrial warehouse is no small feat.

    In this article, we’ll unpack what industrial warehouses are, their types, roles, and the best practices for managing them efficiently in today’s fast-paced, tech-driven world.

    What is an Industrial Warehouse?

    An industrial warehouse is a large, specialized facility used to store goods, raw materials, components, or finished products for industrial use. These aren’t your everyday storage units—they’re built for heavy-duty storage, bulk inventory management, and efficient movement of goods.

    Key Functions of an Industrial Warehouse

    • Storage of goods (raw materials or finished products)
    • Inventory management and stock control
    • Order fulfillment and picking/packing operations
    • Shipping and receiving logistics
    • Buffer for production and market demand

    In short, industrial warehouses keep the wheels of commerce turning.

    Types of Industrial Warehouses

    Let’s explore the main types based on design, function, and use:

    • Distribution Centers (DCs): These are high-throughput facilities where goods move in and out quickly. Think Amazon fulfillment centers.
    • Cold Storage Warehouses: Used for temperature-sensitive products like food, pharmaceuticals, and chemicals.
    • Bulk Storage Warehouses: Ideal for storing large quantities of raw materials such as grains, minerals, or chemicals.
    • Automated Warehouses: These leverage robotics and AI to automate inventory storage, retrieval, and handling.
    • Flex Space Warehouses: Multi-purpose spaces used for storage, manufacturing, and office work. They’re popular with SMEs and startups.
    • Hazardous Material Warehouses: Designed with safety features to store flammable, toxic, or reactive materials.

    Layout and Design Considerations

    The efficiency of warehouse operations depends heavily on its layout. Here’s what matters:

    • Dock design: Separate inbound and outbound docks
    • Aisle width: Must accommodate forklifts or AGVs
    • Storage systems: Pallet racking, shelving, mezzanines, etc.
    • Zoning: Segregation based on product type or handling requirements
    • Safety compliance: Fire exits, safety zones, PPE stations

    A well-planned layout reduces travel time, increases picking accuracy, and boosts productivity.

    Warehouse Management: Core Areas to Master

    Now, let’s get into how to manage an industrial warehouse effectively. These are your key areas:

    1. Inventory Management

    This is the heartbeat of warehouse operations.

    • Use real-time inventory tracking systems (WMS, RFID, barcoding)
    • Avoid overstocking and understocking
    • Implement cycle counting for accuracy
    • Utilize ABC analysis to prioritize high-value items

    2. Order Fulfillment and Picking Strategies

    Efficient picking = faster order processing.

    • Batch Picking: Pick multiple orders at once
    • Zone Picking: Assign zones to different pickers
    • Wave Picking: Group orders based on schedules or routes

    Use pick-to-light or voice picking systems for better accuracy.

    3. Automation and Technology

    Technology is revolutionizing warehouse management:

    • Warehouse Management Systems (WMS) for end-to-end visibility
    • Automated Guided Vehicles (AGVs) for material movement
    • Drones for stocktaking and surveillance
    • IoT Sensors for real-time data on inventory, temperature, etc.
    • AI and analytics for demand forecasting and process optimization

    4. Labor Management

    People still matter—even in automated warehouses.

    • Use labor tracking tools to monitor productivity
    • Train workers regularly on safety and tech use
    • Schedule shifts based on workload forecasts
    • Incentivize performance with KPIs and rewards

    5. Safety and Compliance

    Safety isn’t optional—it’s essential.

    • Conduct regular audits and risk assessments
    • Provide PPE and safety gear
    • Install safety signage, fire suppression systems, and emergency exits
    • Ensure compliance with OSHA, ISO, and local safety standards

    6. Inbound and Outbound Logistics

    This is where delays and losses often happen.

    • Schedule deliveries and pickups to avoid bottlenecks
    • Use dock appointment systems
    • Track shipments using GPS and IoT
    • Integrate your warehouse with TMS (Transport Management Systems)

    Warehouse KPIs to Track

    To manage it well, you need to measure it well. Here are key performance indicators (KPIs):

    • Order accuracy rate
    • Inventory turnover ratio
    • Warehouse capacity utilization
    • Picking accuracy
    • On-time shipping rate
    • Average order processing time

    Best Practices for Industrial Warehouse Management

    1. Go digital – Paper-based tracking is outdated
    2. Regularly audit inventory – Don’t just rely on the system
    3. Optimize space – Use vertical storage and dynamic slotting
    4. Train your team – A skilled workforce is a safe and productive one
    5. Plan for seasonality – Have a game plan for peak periods
    6. Invest in preventive maintenance – Keep your equipment in top shape

    Benefits of Efficient Warehouse Management

    • Faster order fulfillment
    • Lower operational costs
    • Happier customers
    • Better supplier coordination
    • Reduced shrinkage and damage
    • Improved data visibility for strategic planning

    Challenges in Industrial Warehouse Management

    No sugarcoating it—warehouse management comes with its hurdles:

    • Labor shortages
    • Space constraints
    • Supply chain disruptions
    • High tech implementation costs
    • Cybersecurity threats in smart warehouses

    The Future of Industrial Warehouse Management

    The future is smart, connected, and automated. Expect to see:

    • AI-powered warehouse optimization
    • Fully autonomous robots
    • Blockchain for secure inventory tracking
    • Predictive analytics replacing reactive decision-making
    • Green warehouses powered by solar and focused on sustainability

    Conclusion

    Industrial warehouses are no longer just storage spaces—they’re critical hubs that drive supply chain performance. With the right layout, technologies, and management practices, you can transform your warehouse from a cost center into a competitive advantage.

    Efficient warehouse management isn’t just about storing things—it’s about strategically moving, tracking, and optimizing every piece of inventory that enters and exits your building.

  • Industrial Automation: How it Works, Types, and Benefits

    Industrial Automation: How it Works, Types, and Benefits

    Imagine a world where machines take care of repetitive, risky, and time-consuming tasks—while humans focus on creativity and strategy. That’s not the future anymore. It’s happening right now, thanks to industrial automation.

    In today’s highly competitive landscape, automation isn’t just a luxury for big corporations—it’s a necessity for any business that wants to scale efficiently. Let’s break down exactly how industrial automation works, the different types, and the benefits it brings to industries around the world.

    What is Industrial Automation?

    At its core, industrial automation is the use of technologies like machines, control systems, and software to operate industrial processes with minimal or no human intervention. Instead of people doing the heavy lifting, machines do it faster, more accurately, and around the clock.

    How Industrial Automation Works

    Automation systems are made up of several working parts that interact like a well-oiled machine. Here’s how they come together:

    1. Sensors and Input Devices

    These are like the eyes and ears of the system. Sensors collect real-time data such as temperature, pressure, speed, and more.

    2. Controllers (PLC, DCS)

    This is the brain. Devices like Programmable Logic Controllers (PLCs) process the sensor data and make decisions. For example, if a sensor detects overheating, the controller can shut down the machine instantly.

    3. Actuators and Output Devices

    These are the muscles. Actuators perform the physical actions—turning motors, opening valves, or moving arms—based on instructions from the controller.

    4. Human-Machine Interface (HMI)

    The HMI allows operators to monitor and control the system through a user-friendly dashboard or screen.

    5. Software and Communication

    Systems like SCADA and Industrial IoT platforms gather, analyze, and report data for optimization and predictive maintenance.

    Put it all together and you get a seamless system that can run everything from manufacturing lines to power plants.

    Types of Industrial Automation

    Not all automation systems are created equal. They vary based on flexibility, complexity, and application.

    1. Fixed (Hard) Automation

    Used in mass production settings, such as car manufacturing. It’s fast and efficient but lacks flexibility. Once programmed, it’s hard to change.

    2. Programmable Automation

    Great for batch production. Systems can be reprogrammed to handle different tasks. Common in textile and electronics industries.

    3. Flexible (Soft) Automation

    Highly adaptive and ideal for modern industries that require frequent changes. You’ll find this in custom manufacturing and smart factories.

    Top Benefits of Industrial Automation

    Why are companies rushing to automate? The advantages speak for themselves:

    1. Higher Productivity: Machines don’t sleep, get tired, or take breaks. They run 24/7, massively boosting output.
    2. Improved Accuracy and Consistency: Automation reduces human error and ensures every product meets exact standards.
    3. Enhanced Safety: Hazardous tasks can be done by machines, reducing risk for human workers.
    4. Cost Savings: Though initial setup can be expensive, long-term savings come from reduced labor, energy use, and material waste.
    5. Better Data and Insights: Automated systems generate loads of data, which can be analyzed to make smarter, faster decisions.

    Real-World Applications of Industrial Automation

    • Manufacturing: From assembling cars to making smartphones, automation drives efficiency and consistency in factories.
    • Food & Beverage: Sorting, bottling, packaging, and quality control—automation ensures hygiene and accuracy.
    • Pharmaceuticals: Precise dosing, mixing, and packaging are critical here, and automation helps meet strict regulations.
    • Oil & Gas: Automation helps monitor pipelines, detect leaks, and improve worker safety in dangerous environments.
    • Logistics & Warehousing: Automated systems pick, pack, and ship products with blazing speed and accuracy.

    Emerging Technologies in Industrial Automation

    • Robotics: Industrial robots are now smarter, safer, and more collaborative (like cobots).
    • AI and Machine Learning: Machines can now learn from past data and make predictions—like when a machine might fail.
    • Industrial IoT (IIoT): IIoT connects devices and sensors to the internet, providing real-time insights and remote control.
    • Edge Computing: Processing data near the source rather than in a distant cloud reduces delay and increases efficiency.

    Challenges of Industrial Automation

    Nothing is perfect. Here are a few roadblocks:

    • High Initial Cost: Small businesses may find automation expensive to implement upfront.
    • Job Displacement: As machines replace manual tasks, there are concerns about job loss—though new tech jobs are also being created.
    • Cybersecurity Risks: Connected machines can be hacked if not secured properly.
    • Integration Complexity: Merging old legacy systems with modern automation can be tricky and requires expertise.

    Future of Industrial Automation

    The future is hyperautomation—where everything that can be automated will be. We’ll see:

    • Greater human-robot collaboration
    • More use of green automation (sustainable energy use)
    • Smarter systems powered by AI and big data

    The shift will empower businesses to be faster, safer, and more customer-focused.

    Conclusion

    Industrial automation isn’t just changing factories—it’s reshaping the entire economy. By understanding how it works, the types available, and the benefits it brings, businesses can make informed decisions and stay ahead of the curve.